Inventory management software needs a new standard
The old inventory management software promise was visibility: better stock counts, cleaner locations, and fewer surprises. Manufacturers still need that, but today with AI changing what's possible, visibility is the floor.
Stock visibility tells you what the system thinks exists. The next level is manufacturing inventory management, which tells you what can actually be used. Inventory intelligence helps the team decide what should happen next. This article defines those three levels and the bar manufacturers should use when buying inventory management software in 2026.
The problem with a lot of generic inventory software is that it improves the view of stock, but it still leaves the interpretation (i.e., whether it is usable, reserved, consumable, urgent, etc.) to people.
Manufacturers should stop treating inventory visibility as the goal, because today, visibility is a prerequisite. The goal is usable inventory context.
In manufacturing, stock is not a static asset sitting on a shelf. It is a changing constraint. Raw materials become work in progress, work in progress becomes finished goods, and finished goods may be reserved, blocked, relabeled, reworked, shipped, or held back because the customer needs a different remaining shelf life. Every movement can change what planning, purchasing, production, quality, and logistics should do next.
Inventory management software that cannot follow that movement turns experts into translators, showing them the data and then asking them to make the data operational.
It's relatively straightforward to build or buy a system that answers the question "how much do we have?" It is much more challenging to find a system that can tell you not only what you have, but what you can (or should) do with it, and proactively makes those suggestions.
Here are three examples of common situations where simple inventory management software can steer manufacturers astray.
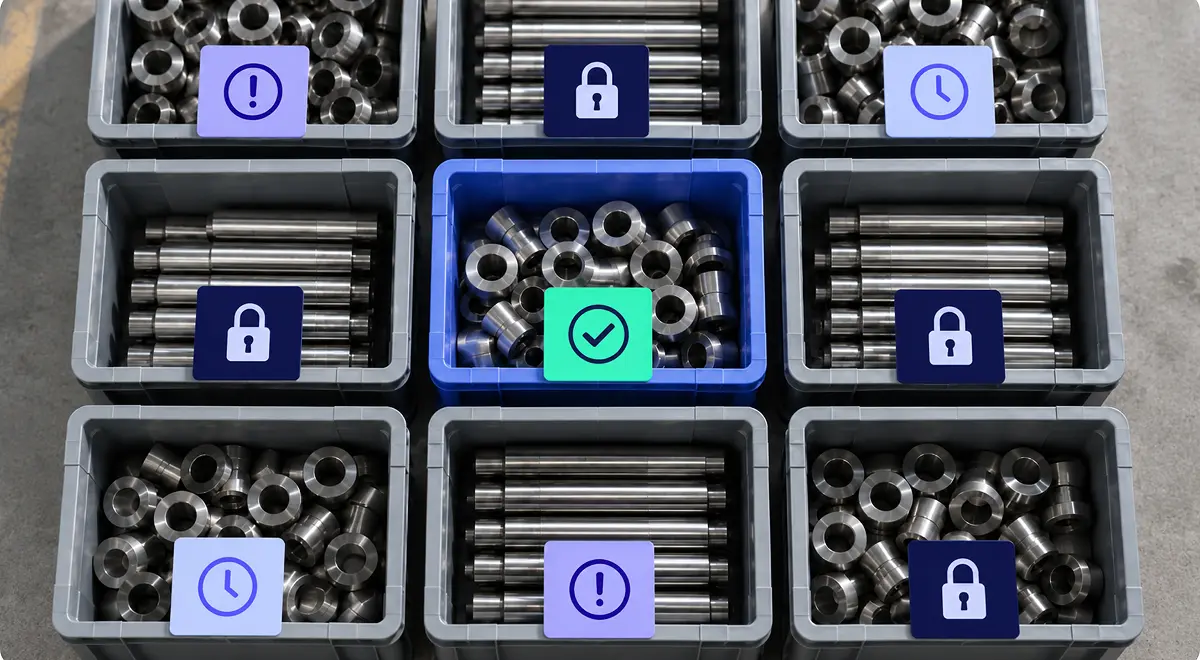
You can have 500 units on hand and still be short. Maybe 200 are blocked by quality, 100 are too close to expiry, 50 are reserved for a strategic customer, and the rest are in a location production cannot reach before the next run. In a retail stock view, that may look available. In manufacturing, it can break the plan.
This is phantom stock: material that appears available in the system but cannot be used when the plan needs it.
Phantom stock is often blamed on warehouse discipline, and sometimes that is fair. In many factories, the deeper issue is that the system does not capture the events that change availability quickly enough. For example, usually production consumption is entered only after the shift, and even scrap is adjusted later.
Good manufacturing inventory management software should separate what the business physically has, what the team can actually use, and what should happen next. Static tools usually stop at the first two. They can report the gap, but they do not help the team resolve it in real time.
Raw material inventory software should do one thing: help buyers prevent shortages before they impact production. Unfortunately, a raw material record alone does not tell the buyer enough.
The real shortage risk depends on demand, bills of materials (BOMs), open purchase orders (POs), supplier lead times, substitutions, quality status, and production timing. If those signals are disconnected, material requirements planning (MRP) will only be so accurate, and it likely will have to be verified manually with the right context.
For a broader look at the planning layer, Bonx's guide to production planning software for manufacturers explains how production decisions change when constraints move. For the data structure underneath it, the guide to BOM management and bill of materials software covers why material logic depends on BOMs that operations can trust.
The standard should be higher than showing stock below a reorder point. A buyer needs to know why the need exists, when the shortage will affect production, whether a substitute is allowed, and whether the recommended purchase is routine enough to prepare automatically or risky enough to review.
At L'Atelier du Ferment, Bonx connects sales demand, production planning, batch traceability, shelf life, and cold storage capacity, so production and purchasing work from the same constraints instead of separate files. That is the difference between raw material inventory as a database and raw material inventory as shortage-prevention logic.
Lot tracking is often sold as a compliance or recall feature. But in daily manufacturing, it also decides what the team is allowed to do. Which supplier lot can be consumed for this production order? Which finished batch can ship to this customer? Which material is blocked, released, waiting for retesting, or too close to expiry?
The audit trail is obviously important, but good lot tracking also keeps the system from suggesting a batch that should not move in the first place.
FIFO, FEFO, and LIFO often get mixed together here. FIFO and LIFO are often discussed as accounting methods, while FEFO is usually about expiry. In manufacturing, the practical question is more immediate: what is the oldest eligible stock for this job, order, or customer?
It's a more complex question than meets the eye, as the oldest batch may be blocked, the earliest-expiring batch may fail a customer's shelf-life rule, and the easiest material to pick may be reserved for tomorrow's production run.
Bonx's guide to FIFO vs. LIFO in manufacturing inventory goes deeper on the difference between physical stock rotation and accounting cost flow. For inventory software, the point is simple: lot tracking should shape decisions in real time, rather than only help the team reconstruct what happened afterward.
AI does not make inventory management better by adding a chatbot to a stock table. A chatbot that answers "what stock is available?" is only as useful as the data behind it. If reservations, quality holds, production consumption, batch status, purchase orders, and customer commitments sit in separate tools, AI can summarize bad data faster, but it will not make the operation more reliable.
AI becomes useful when the inventory system has enough live operating context to turn signals into prepared actions. That can mean detecting shortage risk before a production order is blocked, preparing purchase suggestions from demand and usable stock, explaining why a material need exists, flagging unusable lots, prioritizing cycle counts, or routing exceptions when customer priority, supplier risk, or quality needs judgment.
These are not abstract AI use cases. They are the routine checks experienced people already do. The opportunity is to let the system do more of that checking and preparation, then bring people in where judgment matters.
Bonx is the AI-native manufacturing ERP that was built as a system of action, not just a system of record. It can generate manufacturing orders, prepare procurement suggestions, prioritize stock, surface exceptions, and handle other routine operational work under human oversight when configured to do so. At additive manufacturer Something Added, Bonx groups orders, generates manufacturing orders, and assigns jobs to machines based on industrial constraints, the same operating principle supports 24/7 production with more than 10,000 parts produced each month. The system handles repeatable coordination work so the team can supervise the edge cases.
If you're buying manufacturing inventory software today, you should be focused on questions that zone in on whether it's a system of record, or of action. For example, "Can the software prepare a purchase suggestion, explain which production order will be blocked, flag a lot before someone tries to consume it, ask for approval when the action is risky, and keep a trace of what it did and why?"
If the answer is no, the AI layer may still help with search and reporting. It just will not fundamentally change the operating burden.
Manufacturers should be more skeptical in inventory software demos. Do not be impressed because the interface can show stock by item, location, or batch. That is the old promise. Ask what the system does when the stock position becomes complicated.
If the demo looks good but the team would still need a spreadsheet to decide what is usable, reserved, risky, or urgent, the software is not solving manufacturing inventory management.
Be wary of:
This is the standard manufacturers should bring into every inventory software conversation:
That last layer is where the work changes. A buyer does not need another alert saying a material is low. They need the system to prepare the purchase suggestion, explain why the need exists, and flag the cases where supplier risk or customer priority needs judgment. A planner does not need another stock dashboard; they need to know which production order will be blocked and what can still be changed.
Inventory management software for manufacturing should not make experts stare at better data and keep doing the same reconciliation work. It should turn stock into actual operating decisions, ideally carried out by the system itself with a human for review.
That is the bar in 2026. Visibility is table stakes. Usability is the test. Action is the standard.
Inventory management software for manufacturing helps teams manage stock across raw materials, work in progress, and finished goods. A strong system does more than track quantities and locations. It connects inventory to purchasing, production, quality, traceability, planning, and internal logistics so the team can make better operating decisions.
Retail inventory management usually focuses on what is available to sell or ship. Manufacturing inventory management has to follow stock as it changes form through production, including raw material consumption, WIP, finished goods output, scrap, rework, quality holds, reservations, and lot or batch rules.
Raw material inventory software tracks the materials, components, and packaging used in production. In manufacturing, it should connect raw material stock to supplier lots, quality status, bills of materials, open purchase orders, supplier lead times, substitutions, and production demand so buyers can catch shortages earlier.
MRP depends on inventory accuracy because it calculates what to buy or make from demand, bills of materials, current stock, open supply, and lead times. If inventory is stale, blocked, reserved, or physically wrong, the MRP recommendation may look correct while still being unusable for the factory.
Phantom stock appears when inventory exists in the system but cannot actually be used. Common causes include late production declarations, unrecorded scrap, missing transfers, manual reservations, wrong locations, unit conversion errors, quality holds outside the inventory system, and batch splits that were not captured correctly.
AI can help with inventory management when it has live operating context. Useful applications include shortage-risk detection, procurement suggestions, lot eligibility checks, cycle-count prioritization, variance investigation, exception routing, and explanations for why the system recommends a specific action.
AI cannot fix disconnected or untrusted inventory data by itself. It can help find patterns, flag suspicious movements, and suggest where to investigate, but manufacturing inventory still depends on timely stock movements, production declarations, quality updates, reservations, and purchasing data.
Lot tracking connects materials, production, quality, finished goods, and shipments. It helps the team know which stock can be consumed or shipped, which batches are affected by a quality issue, and which customers or orders may be impacted.
Standalone inventory software can work when the main problem is simple stock control. Manufacturers usually need inventory inside a connected manufacturing ERP when stock affects production planning, purchasing, quality, traceability, customer promises, and internal logistics.
Manufacturers should look for software that handles raw materials, WIP, and finished goods; distinguishes physical stock from usable stock; connects inventory to BOMs, MRP, purchasing, production, quality, and internal logistics; supports lot and batch tracking; explains recommendations; and uses AI to prepare or route actions inside the workflow.


Contact us
So were we. That's why we built Bonx, the AI-native manufacturing ERP.